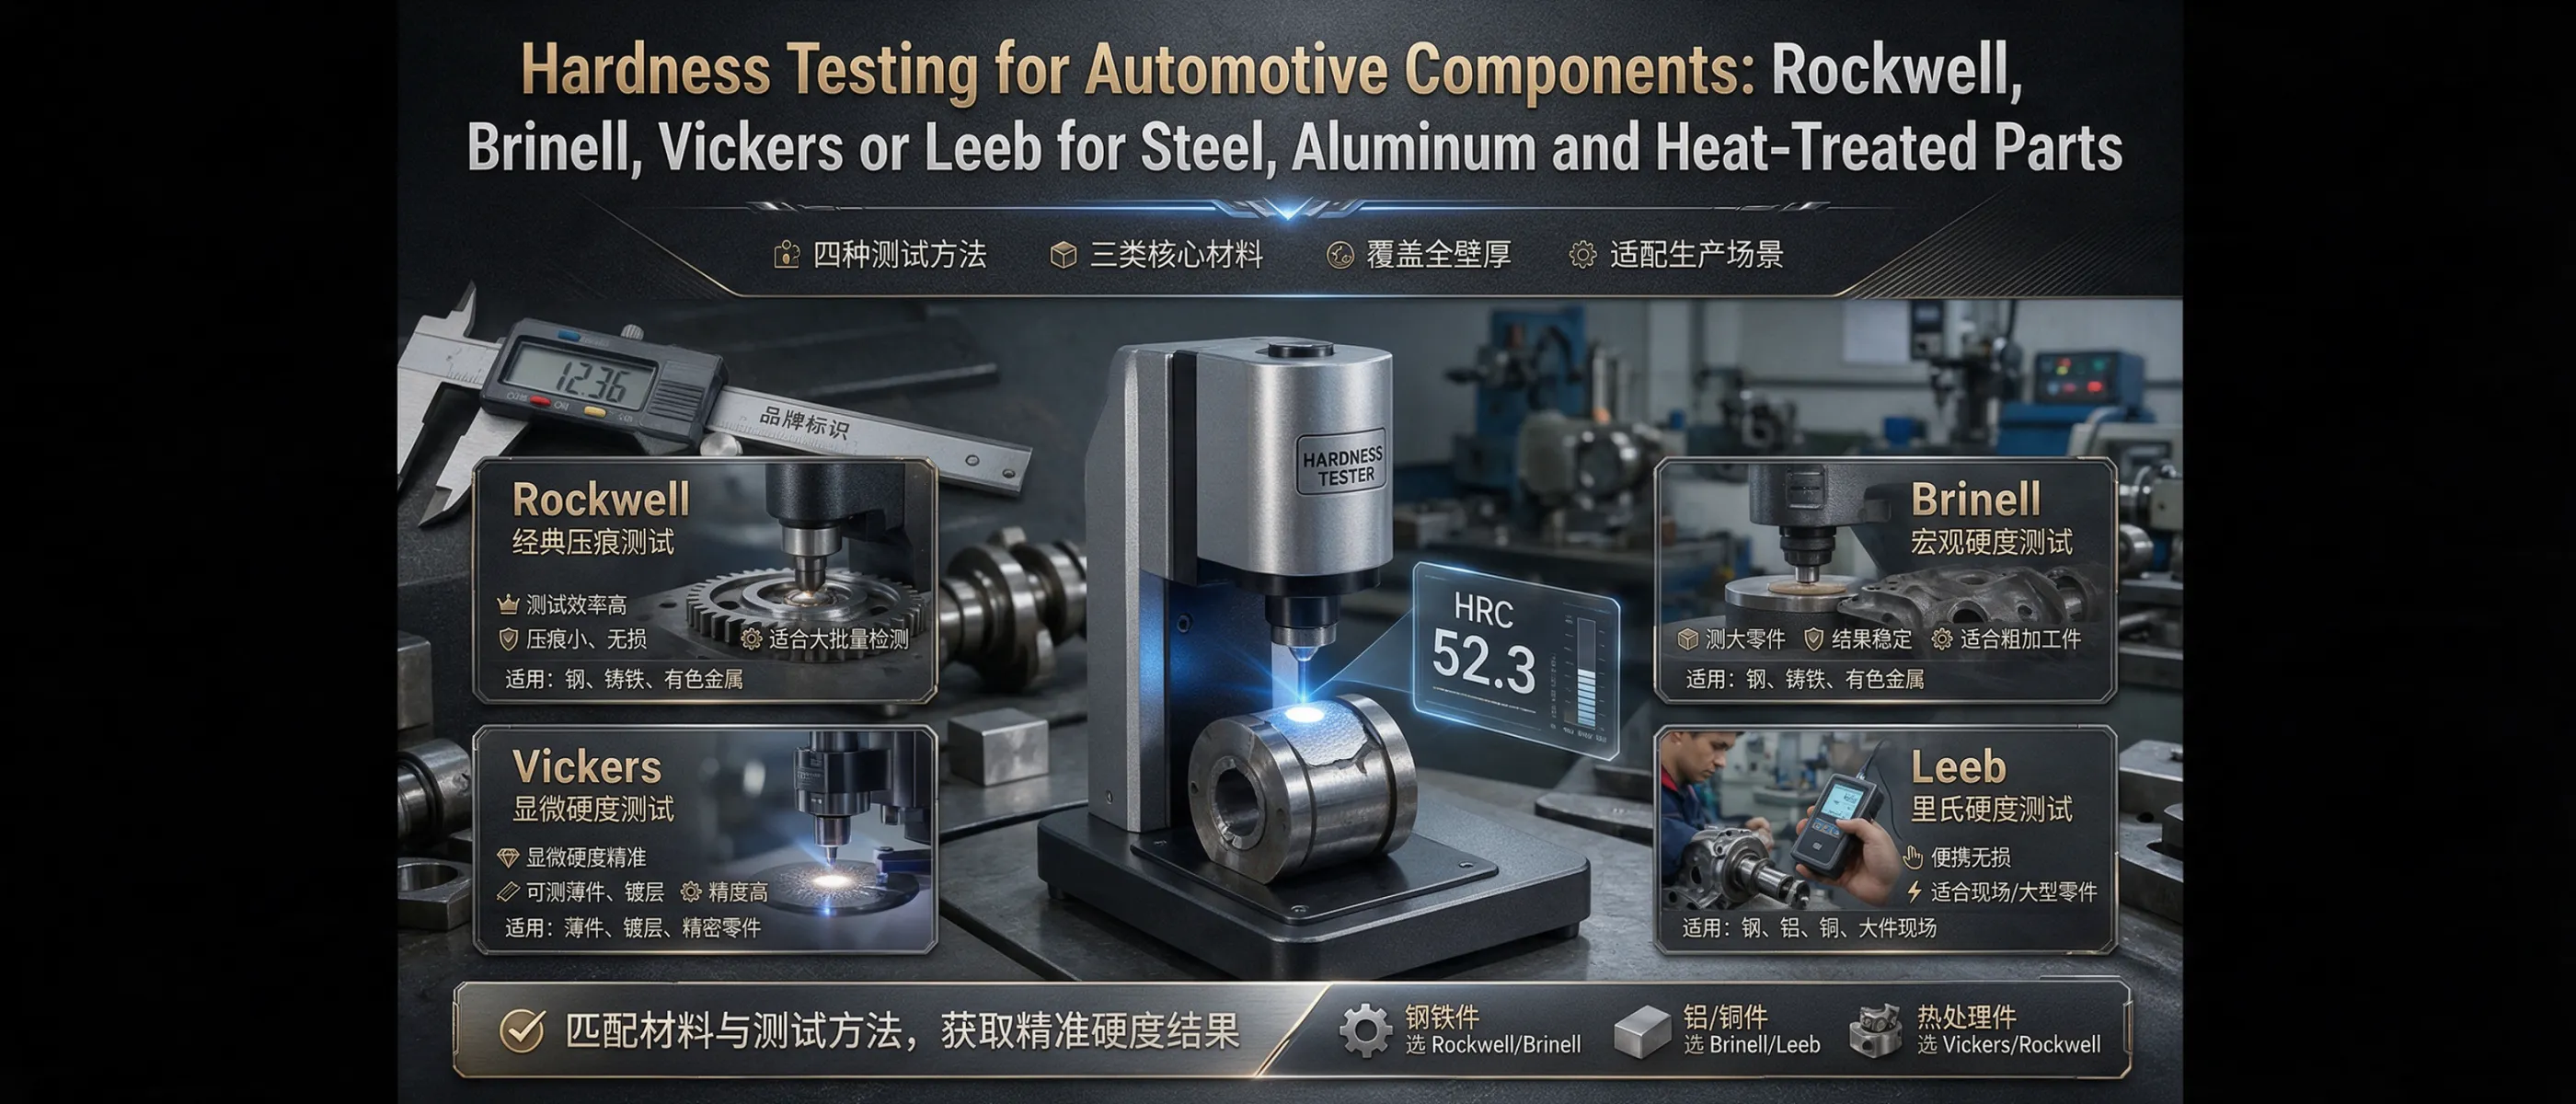
Choosing a hardness tester for heat-treated parts starts with the inspection question: are you checking the hardness of the whole part, a surface layer, or a specific location within a cross-section? Rockwell, Brinell and Vickers tests use different indentation methods, so the right choice also depends on material, geometry, surface preparation and the applicable test standard.
Rockwell hardness is determined from the depth of indentation under specified test forces. It is often considered for routine checks of heat-treated parts when the surface, thickness and support meet the requirements of the selected scale. Different scales use different indenters and forces; the scale must be chosen for the material and expected hardness. Thin layers, small features and curved surfaces require particular attention.
Brinell testing uses a ball indenter and measures the size of the resulting impression. Its larger impression can help assess materials with a relatively coarse or non-uniform structure, provided the test area and part thickness are sufficient. The impression may be unsuitable for small features or finished surfaces where indentation damage is unacceptable. The ball size and force must be appropriate for the material and standard.
Vickers testing uses a diamond pyramid indenter; hardness is calculated from the measured impression diagonals and applied force. Depending on the force and equipment, it can be useful for small features, surface layers and hardness measurements at defined points across a prepared section. Accurate optical measurement requires suitable surface preparation, and fine-scale work may take more preparation and measurement time.
Identify the method and edition required by the drawing, customer specification or inspection plan. Depending on the application, relevant documents may include ISO 6508 or ASTM E18 for Rockwell, ISO 6506 or ASTM E10 for Brinell, and ISO 6507 or ASTM E384 for Vickers. Check the scope and requirements of the applicable document rather than assuming that standards or equipment models are interchangeable.
Hardness values from different methods should not be treated as directly equivalent. Where conversion is permitted, use an applicable conversion standard or agreed procedure, confirm its material and range limitations, and report the original result and any converted value clearly.
Before requesting a recommendation, assemble the part material, heat-treatment details, expected hardness, dimensions, test location, required standard and daily sample volume. Also note whether testing must take place on the production floor and whether records or automated measurements are needed.
Use those conditions to compare candidate testers, then confirm the supported scales or forces, indenter options, workpiece capacity, measurement functions and verification requirements against each model’s formal technical documentation. Check the instrument with appropriate reference blocks as required by the applicable procedure, and arrange calibration and maintenance according to the relevant standard and manufacturer’s instructions.